Reviewing the Product Before Manufacturing
The customer provided 3D CAD files, 2D drawings, a BOM and surface-finish requirements. Before production, our technical team reviewed both the individual parts and the complete assembly.
For the ABS housings, we considered machining access, wall thickness, part stability and the amount of material that would need to be removed. We also reviewed the joining edges, external openings and areas that would remain visible after assembly.
The internal aluminum components had to align with the plastic enclosure. Hole positions, mounting features, threads and available clearances were therefore checked in relation to the surrounding parts rather than as isolated dimensions.
We also reviewed the silicone seal grooves and assembly sequence. This helped us identify areas where paint, anodizing or seal compression could affect the final fit.
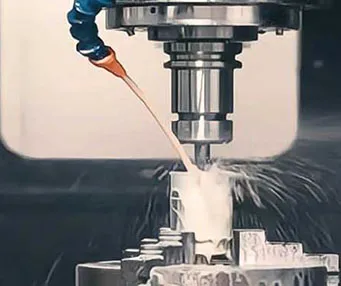
CNC Machining the ABS Housings
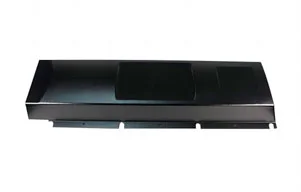
The upper housing, lower housing and other exterior parts were machined from ABS blocks. For 15 sets, CNC machining provided an efficient way to produce functional housings without investing in injection mold tooling at this stage.
ABS is suitable for many electronic product prototypes because it can be machined, sanded and painted to create an appearance close to a molded product. However, machining a cosmetic housing requires careful control. Thin walls may deform, and tool marks or setup transitions can remain visible after painting if the surface is not properly prepared.
After machining, the housings were manually finished and sanded. Particular attention was given to curved surfaces, joining edges and openings. The aim was to remove machining marks while preserving the dimensions of mating and locating features.
Custom Painting and Surface Inspection
The prepared housings were painted in the color specified by the customer. Coating thickness was controlled around assembly edges, holes and openings because excessive paint buildup could change the fit between components.
Once the coating had cured, every housing was checked for:
· Scratches, dents and remaining sanding marks
· Dust, pinholes and other surface contamination
· Uneven color, gloss or texture
· Insufficient paint coverage
· Paint buildup along edges and openings
· Color differences between matching parts
The finished housings were protected during subsequent handling and assembly. This was important because repeated fitting or contact between parts could damage the painted surfaces.
Aluminum Components and Anodizing
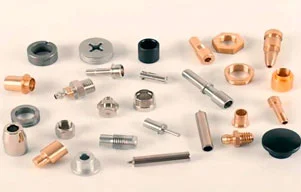
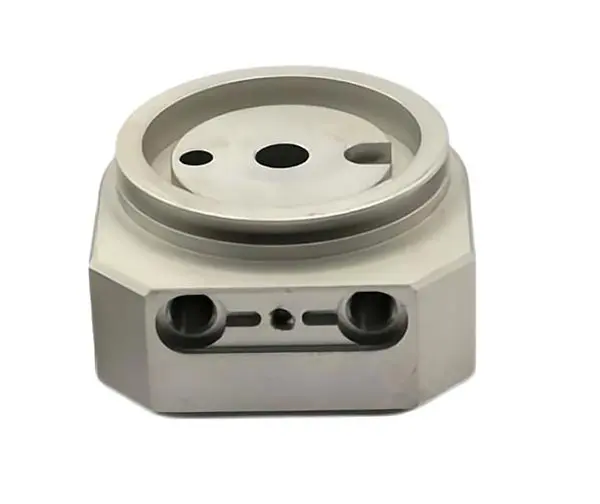
The internal structural and mounting parts were CNC machined from aluminum alloy. These components supported the product assembly and located other parts inside the enclosure.
Before anodizing, we inspected the hole positions, threads, mounting surfaces and mating dimensions. Where a close fit was required, the machining plan allowed for the effect of the anodized layer.
The parts were inspected again after finishing to confirm that threads and functional surfaces remained usable and that the components could be installed without forcing or modifying the surrounding ABS parts.
Silicone Seals Made with Compression Molds
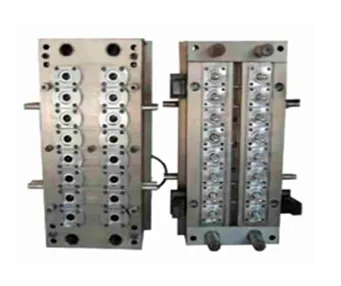
Several custom silicone sealing rings were required inside the product. Dedicated compression molds were made to produce these flexible components.
The molded seals were checked for dimensional accuracy, flash, incomplete filling, deformation and surface damage. During trial assembly, we verified that each seal sat correctly in its groove and remained in position while the housings were closed.
The fit of a silicone seal depends on more than its outside dimensions. The groove size, seal cross-section and available compression all influence whether the enclosure can be assembled properly. For this reason, the seals were evaluated together with the surrounding plastic parts.
Fit Checking and Prototype Assembly
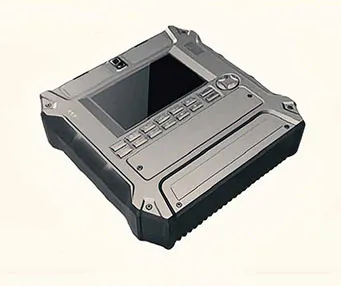
Once the individual components had passed inspection, we assembled the first complete unit. This initial build was used to verify how the plastic housings, aluminum parts and silicone seals worked together.
The assembly check covered:
· Alignment of the upper and lower housings
· Gaps and steps along visible joining lines
· Position of external openings
· Alignment of screw holes and mounting points
· Installation of internal aluminum parts
· Placement and compression of the silicone seals
· Condition of the painted surfaces
· Overall appearance of the finished product
Completing one trial assembly first allowed us to address minor fitting issues before building the remaining units. It also reduced unnecessary disassembly, which could damage painted surfaces or plastic fastening features.
After the fit had been confirmed, the same assembly procedure was followed for the other 14 sets.
Final Inspection and Packing
All 15 assemblies received a final inspection before shipment. We checked the component quantities, critical dimensions, coating quality, color consistency, assembly condition and overall appearance.
Each unit was packed separately to prevent rubbing, impact and surface damage during international transportation. The completed order was then shipped to the customer in the United States.
Rapid Prototyping for Multi-Part Products
A multi-part prototype often involves more than one manufacturing process. Plastic housings may require CNC machining and painting, while internal metal components need different machining and finishing operations. Flexible seals, buttons or gaskets may require separate tooling.
YS Rapid provides rapid prototyping and manufacturing support for projects that combine different materials and processes. Depending on the product design and development stage, we can coordinate CNC machining, turning, silicone compression molding, urethane casting, sheet metal fabrication, painting, anodizing, printing and light assembly.
For overseas engineering teams looking for rapid prototyping in China, this coordinated approach helps reduce the communication and assembly risks that can arise when components are purchased from several unrelated suppliers.
Discuss Your CNC Rapid Prototype
To review a new project, customers can provide 3D CAD files, 2D drawings, material requirements, quantities, surface specifications and any important assembly information.
Our team will evaluate the parts, clarify technical details and recommend a suitable manufacturing route before production. Whether the requirement is for individual components or a complete prototype assembly, we can support the project from file review and prototype manufacture through finishing, inspection and international delivery.
 EN
 jp
 ko
 fr
 de
 es
 it
 pt
 tr
 ar
 iw